What Are The Benefits Of Heavy Vibrating Screen
Heavy vibrating screens are essential tools in various industries. They help separate materials effectively. Understanding their advantages can help businesses optimize their processes. Let’s dive into the key benefits of heavy vibrating screens.
Heavy vibrating screens are essential tools in various industries. They help separate materials effectively. Understanding their advantages can help businesses optimize their processes. Let’s dive into the key benefits of oil burners.
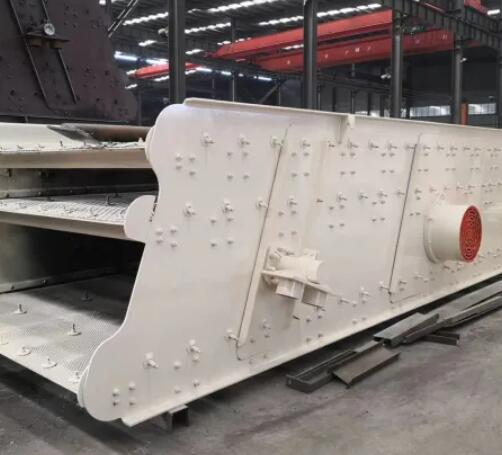
1. Enhanced Material Separation
First and foremost, heavy vibrating screens provide superior material separation. The vibrating motion allows for the efficient sorting of materials by size.
*“How does that work?”* you may ask. Well, the screen’s vibration helps smaller particles pass through while keeping larger ones on top. This ensures a cleaner, more accurate separation.
2. Increased Efficiency
Next up is efficiency. Heavy vibrating screens operate at high speeds. This means they can process large volumes of material quickly.
Imagine a busy construction site. Workers need to sift through tons of gravel. A heavy vibrating screen can manage this task in a fraction of the time it would take manually. This time-saving feature can greatly improve productivity.
3. Durability and Longevity
Durability is another critical benefit. Heavy vibrating screens are built to withstand tough conditions. They often face rough handling and harsh environments.
*“What about wear and tear?”* you might wonder. These screens are designed with heavy-duty materials that resist wear. This means fewer replacements and lower maintenance costs over time.
4. Versatile Applications
Heavy vibrating screens are versatile. They can be used in various settings, from mining to recycling.
*“So, they can handle anything?”* Yes! These machines are effective for sand, gravel, coal, and even waste materials. This adaptability makes them a valuable asset for any business.
5. Easy Operation and Maintenance
Operating a heavy vibrating screen is straightforward. Many models come with user-friendly controls.
* “Do I need special training?”* Not really. Most operators can learn to use these machines quickly.
Maintenance is also simple. Regular check-ups and basic cleaning are usually all that’s needed. This means less downtime and more effective use of resources.
6. Cost-Effectiveness
Next, let’s talk about cost-effectiveness. Although the initial investment can be significant, the long-term savings are notable.
*“How?”* By reducing labor costs and enhancing efficiency. Businesses see a return on investment in no time. This makes heavy vibrating screens a smart economic choice.
7. Improved Safety
Lastly, using heavy vibrating screens can enhance safety. Manual sorting is risky. Workers may face injuries from heavy lifting or exposure to hazardous materials.
*“But how do the screens help?”* By automating the sorting process, risks are minimized. This leads to a safer work environment and increased employee satisfaction.
Conclusion
In summary, heavy vibrating screens offer multiple benefits. They enhance material separation, increase efficiency, and are durable. Their versatility allows for a wide range of applications, making them a wise investment. Plus, they are easy to operate and maintain, leading to cost savings and improved safety.
If you’re considering adding heavy vibrating screens to your operation, contact us for more information. Our experienced team can assist you in finding the right solutions. Reach out to a reliable heavy vibrating screen supplier today!